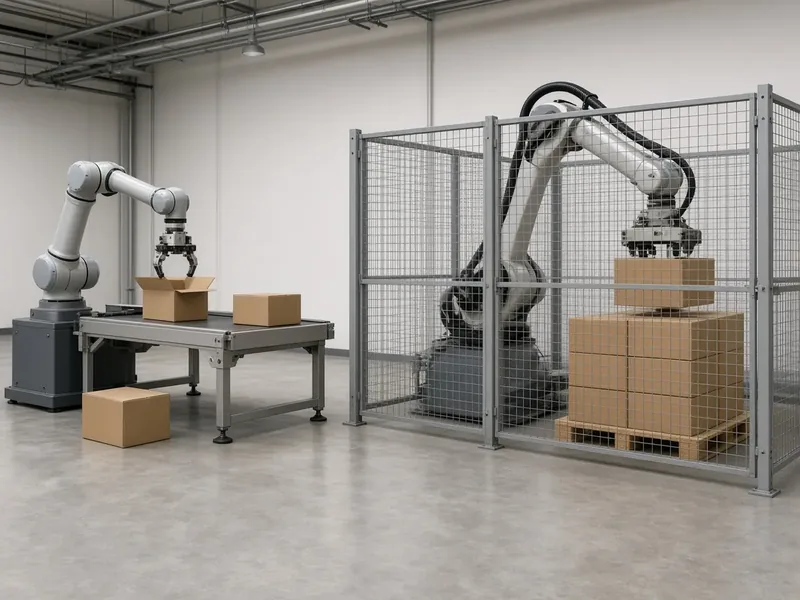
Use this secondary packaging line footprint planner to calculate exact floor length × width (m²) and zero-pressure MDR accumulation conveyor length (45–90 s buffer) across separate inline lines, 90° U-cells, and space-saving LV-P200-MP monoblock packer-palletizers (-40% area).
Robotic Kinematics (4-Axis Delta vs 6-Axis Articulated) & Monoblock Integration
Robotic case packing cells (LV-RD120 and LV-RP200) and single-frame monoblocks (LV-P200-MP) replace fixed mechanical linkages with programmable servo paths—allowing one cell to orient, collate, load, and even palletize multiple SKUs inside a compact footprint. Model your floor space in our secondary packaging line footprint planner and apply three kinematic rules:
- 4-Axis Parallel Delta (
LV-RD120,60–120 picks/min) vs 6-Axis Articulated Arm (LV-RP200,8–16 cycles/min): High-speed flexible flow-wraps, pouches, and thermoformed trays under3.0 kgarriving in random orientation on a belt require a carbon-fiber 4-axis Delta spider robot guided by aKeyence/Cognex2D conveyor-tracking camera. Heavy full-layer payloads (10–50 kg), jugs, or cells that alternate between case loading and palletizing require a 4/6-axis articulated robot arm (LV-RP200). - 40% Floor Footprint Reduction with Monoblock Integration (
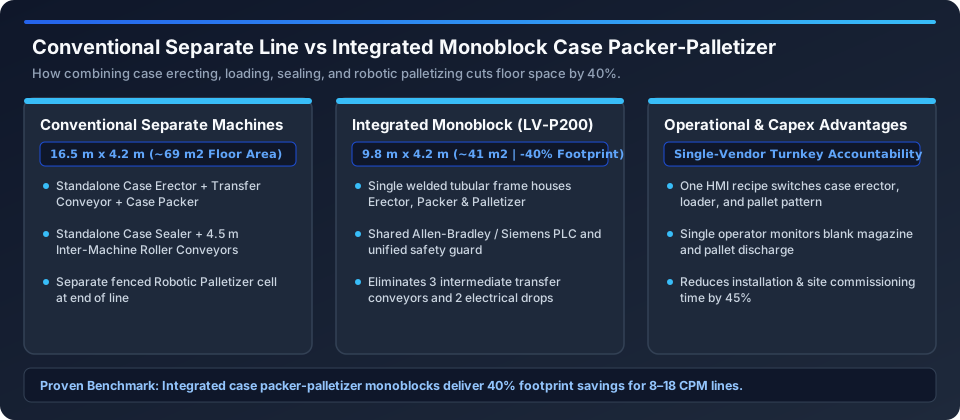
LV-P200-MP): A conventional inline secondary line (separate case erector + conveyor + case packer + conveyor + sealer + accumulation + palletizer) consumes14 to 18 metersof length (~52 m²). Combining case erecting, loading, sealing, and robotic palletizing into one common-chassis monoblock (LV-P200-MP) shrinks the cell to6.5 to 8.5 meters(~30 m²,-40%floor area) under one PLC and safety circuit. - 5-to-10 Minute Tool-Less Recipe & EOAT Changeover: Because pitch spacing, layer rotation (
90° / 180°), and drop depth are stored inAllen-BradleyorSiemensrobot recipes, operators switch SKUs on the touchscreen HMI and snap on quick-release pneumatic EOAT plates in5 to 10 minutes.
Compare related configurations and sizing tools across robotic case packing systems, case erectors and case sealers, automatic case packers, integrated case packer and palletizer monoblock, compact small-footprint case packer, secondary packaging line integration.
End-of-Arm Tooling (EOAT), Vision Tracking & Safety Interlocks
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| Robotic Cell Architecture | LINEVO Series | Rated Speed & Payload | Vision & Collation Method | Ideal Plant Application |
|---|---|---|---|---|
| 4-Axis Delta Vision Cell | LV-RD120 |
60–120 picks/min (≤3 kg pick) |
2D camera conveyor tracking + encoder belt | Randomly oriented pouches, flow-wraps, bakery & frozen trays (12–25 CPM) |
| 6-Axis Articulated Packer | LV-RP200 |
8–16 cycles/min (25–65 kg layer) |
Servo race-track or lane collator + full-layer EOAT | Heavy multipacks, jugs, cans, and multi-SKU contract packaging (10–22 CPM) |
| Cobot Dual-Role Packer | LV-CP12 |
6–10 cycles/min (12–25 kg payload) |
Fenceless dual-zone floor laser scanner (ISO/TS 15066) |
Low-to-medium speed lines (4–10 CPM) with tight aisle clearance |
| Monoblock Packer-Palletizer | LV-P200-MP |
8–16 CPM (-40% floor footprint) |
Integrated Erect + Pack + Seal + Palletize in one frame | Brownfield plants automating case packing and palletizing in <8.5 m length |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
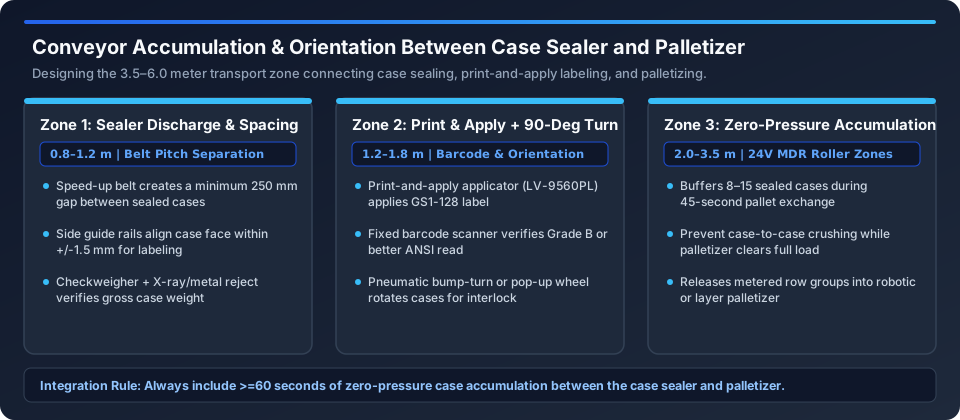
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Request a 2D/3D CAD floor layout