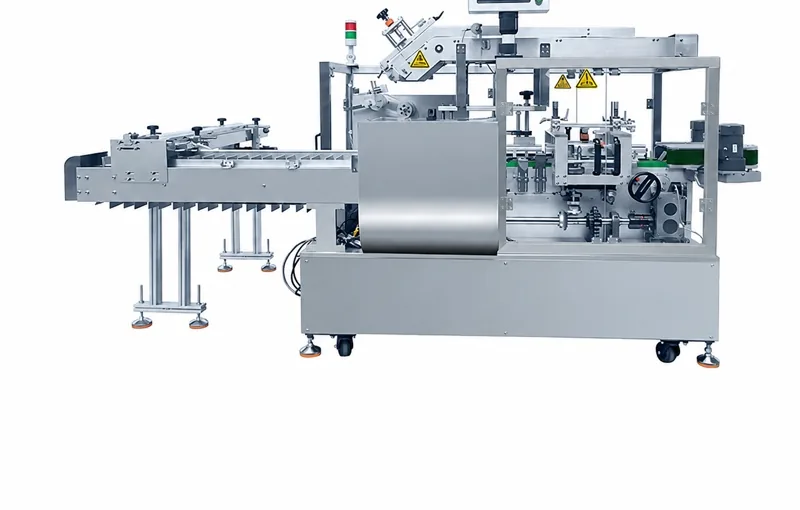
Engineering a LINEVO LV-P200 horizontal side-load (15–25 CPM) or LV-P270 vertical bottom-load (10–18 CPM) case packer allows rigid folding cartons, pharmaceutical boxes, and canisters to accumulate and load smoothly with 10–15 minute tool-less Siko digital changeovers.
Horizontal Side-Load vs Bottom-Load Up-Stacking Kinematics
Rigid folding cartons, pharmaceutical tuck-end boxes, gable-top cartons, and composite canisters accumulate cleanly against flighted or low-backpressure conveyors, allowing direct mechanical transfer without overhead robot arms. Run your upstream cartoner speed (cartons/min) and case matrix (R × C × L) through our case packer speed and collation calculator and evaluate three mechanical boundaries:
- Horizontal Pusher Force vs Carton Sidewall Stiffness (
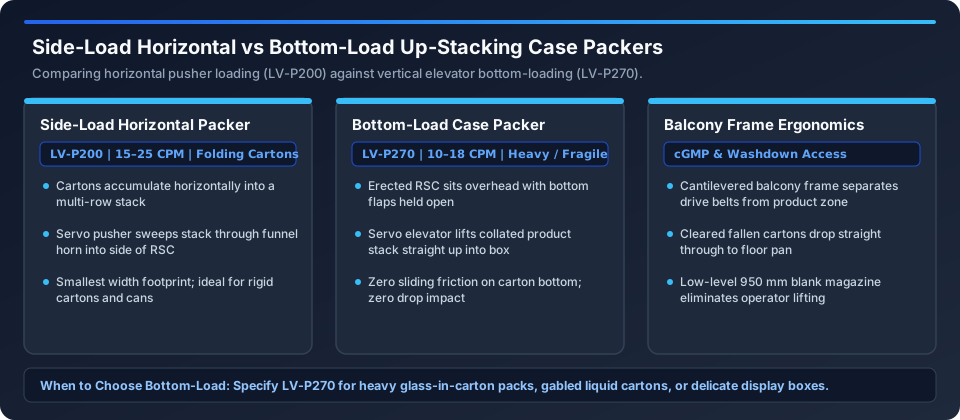
LV-P200,15–25 CPM): On a horizontal side-load case packer (LV-P200), a servo up-stacker builds the multi-layer matrix and a horizontal pusher plate sweeps the completed group through a stainless loading funnel horn into a side-open RSC. This compact balcony architecture handles85%of food, pharmaceutical, and personal-care folding cartons. - Zero-Friction Bottom-Load Elevators for Heavy or Delicate Packs (
LV-P270,10–18 CPM): When packing heavy glass-in-carton bottles, wet gable-top liquid bricks, or high-gloss cosmetic boxes that scuff under horizontal sliding pressure, theLV-P270bottom-load packer erects the RSC overhead and lowers it straight over the collated stack—eliminating horizontal shear and supporting100%of the load from underneath. - 15-Minute Tool-Less SKU Changeover (
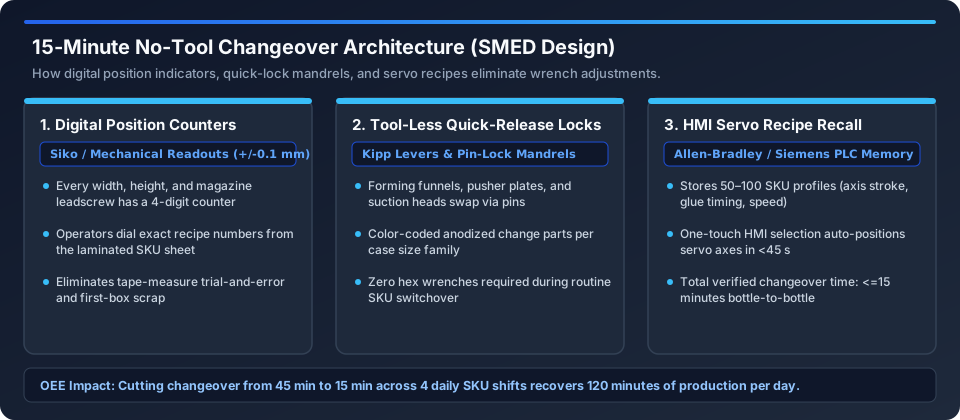
SikoCounters + Servo Recipes): High-mix contract packagers and pharmaceutical lines switching carton sizes4 to 8 times per shiftuseSiko4-digit digital leadscrew indicators (±0.1 mmrepeatability), tool-less Kipp cam levers, and quick-release funnel horns to complete a full 3-dimensional changeover in10 to 15 minuteswith zero hex wrenches.
Compare related configurations and sizing tools across automatic case packers, folding carton side-load case packer, bottom-load vs side-load case packer, semi-automatic hand-pack station, 15-minute no-tool changeover case packer design.
Balcony Frame Architecture, Flap Control & Serialization Aggregation
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| Subsystem Parameter | Side-Load Horizontal (LV-P200, 15–25 CPM) |
Bottom-Load Up-Stacking (LV-P270, 10–18 CPM) |
Plant Engineering Advantage |
|---|---|---|---|
| Product Loading Vector | Horizontal servo sweep through 4-walled loading horn | Vertical elevator lift into overhead erected RSC | Matches pusher force to carton sidewall crush strength |
| Frame & Cleanout Access | Cantilever balcony drop-through stainless frame | Open-front walk-in stainless balcony frame | Crushed cartons or glue debris fall straight to floor tray; 3-min line clearance |
Vision & Aggregation (DSCSA) |
Layer-camera 2D DataMatrix read before horizontal push | Bottom/top camera read + auto-reject before vertical lift | 100% parent-child carton-to-case GS1-128 aggregation (LV-9560PL) |
| Flap Sealing & Squareness | Nordson/Robatech hot-melt or LV-FXC4030X BOPP tape |
Side-belt compression + bottom flap folder before taping/gluing | Guarantees ±1.0 mm case squareness for stable downstream palletizing |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Check my carton collation & speed