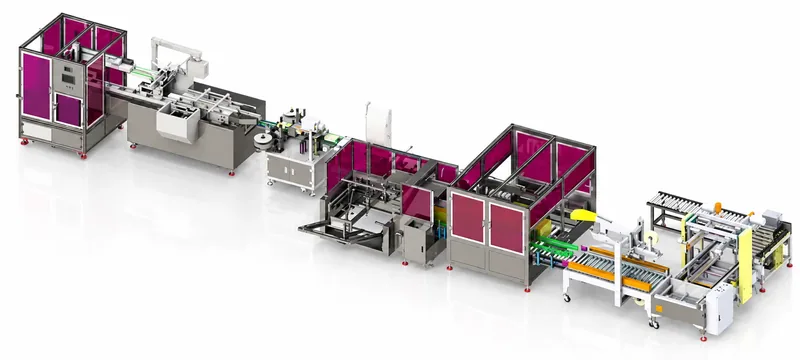
Integrating a turnkey LINEVO erect-pack-seal-palletize secondary packaging line unifies primary discharge conditioning, case erecting, loading, hot-melt/tape sealing, LV-9560PL GS1-128 case labeling, 60-second MDR accumulation, and robotic palletizing under one PackML control architecture.
Synchronizing Case Sealing, GS1-128 Labeling, Accumulation & Palletizing
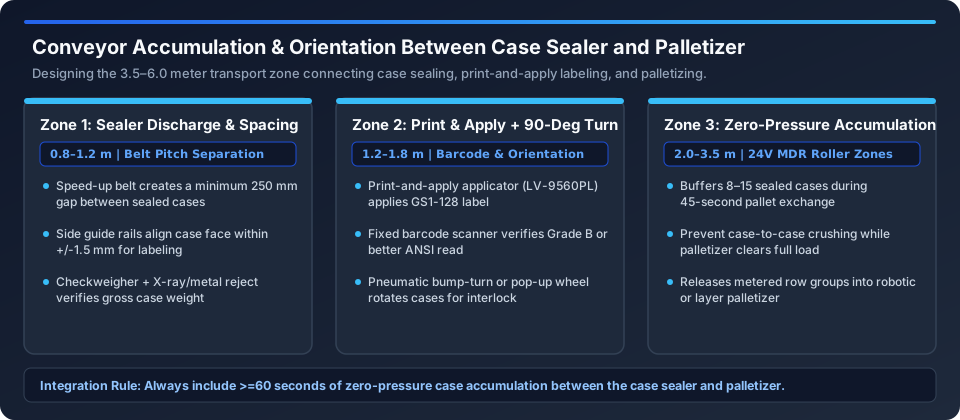
An automatic case packer cannot achieve its rated shift OEE if downstream bottlenecks—such as a label roll change, a pallet exchange pause (45 seconds), or a stretch-wrapper cycle—back up cases into the sealer discharge. Plan your complete end-of-line layout in our secondary packaging line footprint planner and enforce three integration standards:
- 60-Second Zero-Pressure MDR Accumulation Buffer: Between the case sealer discharge (
LV-FXC4030X/LV-HM400) and the palletizer infeed, LINEVO installs3.5 to 6.0 metersof24Vmotorized drive roller (MDR) zero-pressure accumulation conveyor. When the palletizer pauses for30–45 secondsto discharge a full pallet and dispense an empty wood pallet (LV-PD10), the case packer continues running at100%speed without stopping the upstream filler. - Inline Print-and-Apply GS1-128 Case Labeling (
LV-9560PL): Immediately after flap sealing and checkweighing, a servo tamp-blow or corner-wrap print-and-apply labeler (LV-9560PLwithZebraZE511orSatoS84-ex300 DPIthermal-transfer engine) applies serialized GS1-128 labels (32 mmfrom base,≥19 mmfrom vertical edge) and verifiesISO/IEC 15416 Grade B (≥2.5)barcode readability via fixed-mount scanner. - Matching Robotic (
LV-RP200) vs High-Level Layer (LV-HL300) Palletizers: For6–25 CPMlines or multi-line central cells, a 4-axis robotic palletizer (LV-RP200) with vacuum, side-clamp, or bottom-fork EOAT stacks cases to±1.5 mmaccuracy. Above25–50+ CPM, a high-level row-forming stripper-apron palletizer (LV-HL300) forms and squares full layers continuously.
Compare related configurations and sizing tools across automatic case packers, case erectors and case sealers, palletizers for case packing lines, integrated case packer and palletizer monoblock, automatic case packer manufacturer.
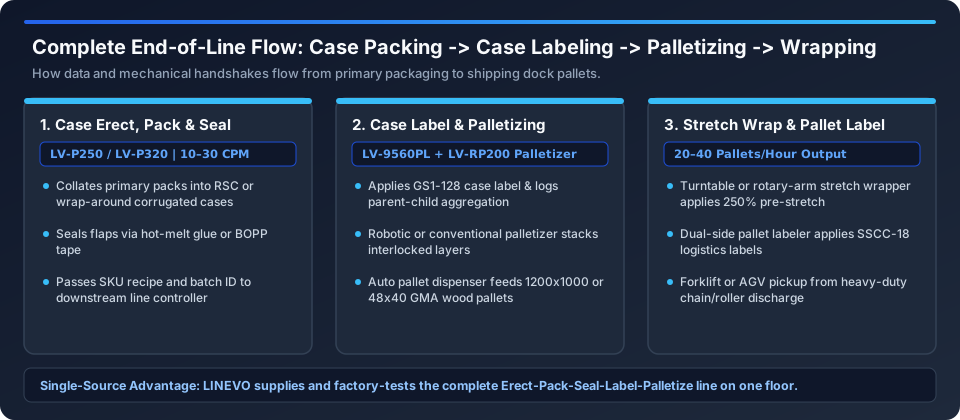
Turnkey End-of-Line Handshake Architecture & Single-OEM FAT Protocol
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| End-of-Line Module | LINEVO Model | Speed Envelope | Mechanical & Data Handshake | Turnkey Integration Benefit |
|---|---|---|---|---|
| Print-and-Apply Case Labeler | LV-9560PL |
15–40 CPM |
Encoder-tracked wipe/tamp/corner-wrap + inline barcode verifier | Zero unverified GS1-128 cases reach the palletizer |
| MDR Accumulation & Turning | LV-MDR60 |
60–90 s buffer |
Photo-eye zoned 24V zero-pressure rollers + bump-turn orientation |
Absorbs pallet exchanges without stopping case packer |
| Robotic / Layer Palletizer | LV-RP200 / LV-HL300 |
8–50+ CPM |
Automatic pallet dispenser (LV-PD10) + slip-sheet inserter |
Stacks column or interlock Ti-Hi patterns within ±1.5 mm |
| Rotary Ring Stretch Wrapper | LV-SW40 + LV-PL100 |
20–45 pallets/hr |
250% powered pre-stretch + 2-panel SSCC-18 pallet labeler |
Delivers dock-ready, retailer-compliant unit loads |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Request a turnkey line layout drawing