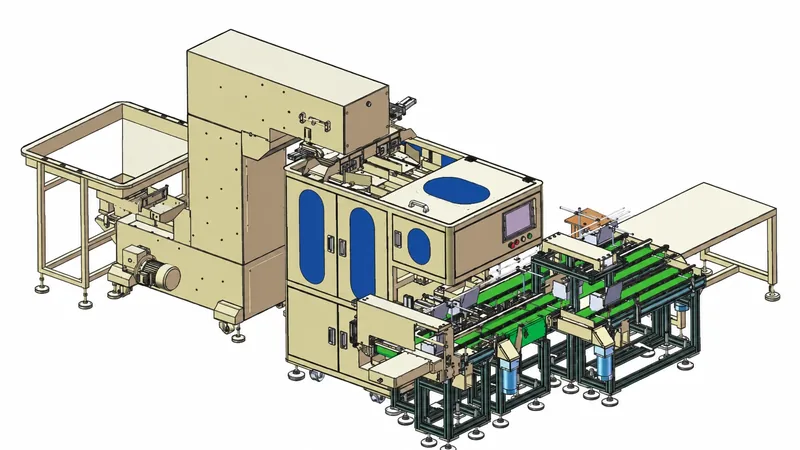
LINEVO Engineering Specification & Verification Protocol
Every machine rating, cycle-time formula, corrugated board tolerance, and floor layout published on AutomaticCasePacker.com is governed directly by the LINEVO Engineering Review Board. Unlike generic equipment directories that quote theoretical dry-cycle speeds, LINEVO publishes net production ratings verified under load on physical packages and knocked-down corrugated blanks inside our assembly plant. Review our automatic case packer home and automatic case packers specifications to see how these standards apply across every machine series.
| Verification Domain | LINEVO Engineering Standard | Physical Proof & Audit Method |
|---|---|---|
Speed & Cycle Ratings (CPM) |
Distinguishes steady net CPM, OEE-derated running CPM (75–84%), and +20–25% surge capacity (LV-P250, LV-P320, LV-P3103) |
Measured during 30-minute continuous FAT production runs under full product load |
| Corrugated & Adhesive Tolerances | Grounded in FEFCO 0201 (RSC) and FEFCO 0409 (wrap-around), 32–48 ECT flute crush, and Nordson/Robatech hot-melt specs |
Tested on 30–50 customer corrugated blanks across ±4 mm humidity warp limits |
| Interactive Engineering Calculators | Deterministic kinematics, blank surface area (m²), and OEE surge math with zero hidden multipliers |
Audited by LINEVO mechanical and controls engineers across tools C11, C12, C13, and C14 |
How LINEVO Rates Machine Speeds, Changeover & Collation Kinematics
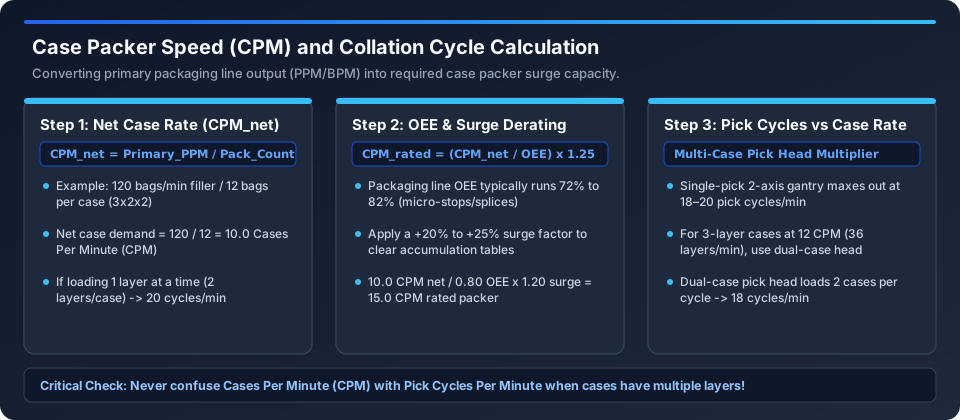
To protect plant engineers from undersized secondary packaging equipment, every technical specification on this site enforces three non-negotiable engineering rules. See how we apply these rules in about LINEVO secondary packaging and our case packer FAT checklist and jam troubleshooting manual:
- Primary-to-Secondary Surge Sizing (
+20% to +25%): A case packer rated at exactly the nominal speed of an upstream VFFS bagger or liquid filler will cause chronic high-level backup stops whenever a magazine is reloaded or a minor carton jam is cleared. Every LINEVO speed table and calculator (C11) automatically applies anOEE factor (0.75–0.84)and a1.20–1.25 surge multiplierto compute required nameplateCPM. - Pick Cycles vs Completed Cases (
CPM): On multi-layer top-load (LV-P250, up to20 CPM) and robotic (LV-RD120,60–120 picks/min) case packers, dividing pick cycles per minute by the number of layers per case determines true case throughput. When a pack pattern exceeds18–22 picks/minon a single head, LINEVO specifies dual-pick tooling (picking 2 layers simultaneously) or twin-head gantries rather than inflating single-head cycle claims. - Documented Tool-Less SMED Changeover (
≤15 Minutes): Changeover times published forLV-P250,LV-P200,LV-P320, andLV-P3103represent complete bottle-to-bottle or pouch-to-pouch SKU transitions executed by one technician usingSikodigital leadscrew counters, quick-release pin mandrels, and HMI servo recipe recall—verified until the first discharged case meets±1.5 mmdiagonal squareness.
Corrugated Board & Sealing Verification Benchmarks
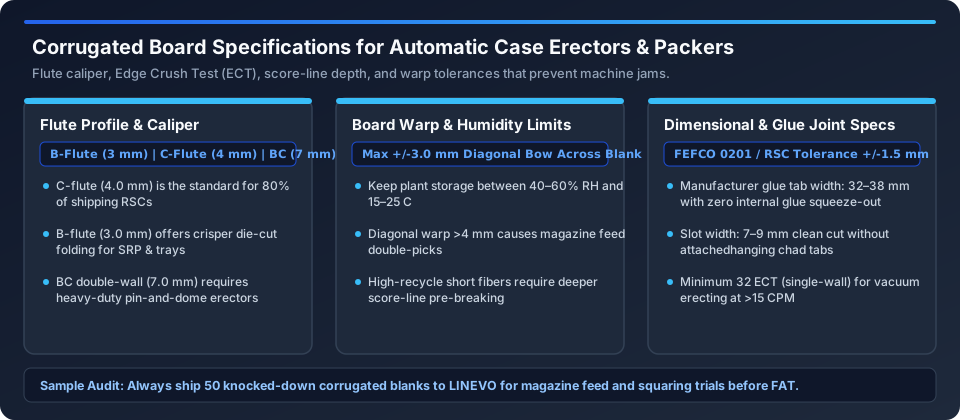
Because 100% recycled testliner and high-humidity warehouse storage introduce blank warp and surface porosity, LINEVO tests every erecting and sealing subsystem against worst-case plant board conditions:
| Subsystem Parameter | Standard Virgin Board Specification (LV-CE150) |
Heavy-Duty Recycled & High-Speed Spec (LV-CE250 / LV-P320) |
Plant Reliability Standard |
|---|---|---|---|
| Blank Opening & Squaring | Single-side Venturi suction (8–12 CPM) |
Dual-frame opposition vacuum or positive pin-and-dome (15–25+ CPM) |
Zero blank slip on porous 100% recycled linerboard and ±4 mm diagonal warp |
| Flute & Board Strength | C-Flute (4.0 mm) or B-Flute (3.0 mm), 32 ECT |
B, C, E, or BC double-wall (3.0–7.0 mm), 32–48 ECT |
Over-breaking score plows (115° fold) eliminate spring-back and corner dog-ears |
| Flap Sealing Method | 48 mm or 72 mm BOPP pressure-sensitive tape (LV-FXC4030X) |
Nordson or Robatech metallocene hot-melt glue (1.0–2.0 s compression) |
Structural fiber-tear bond (≥80% across all 4 flaps) with 35–50% lower consumable cost |
| SMED No-Tool Changeover | Manual crank with engraved millimeter scales (15–20 min) |
Siko 4-digit mechanical counters + quick-release pins + PLC recipe (≤15 min) |
First case out after SKU switch is square within ±1.0 mm; zero hex wrenches required |
Mandatory 4-Gate Pre-Shipment FAT Protocol
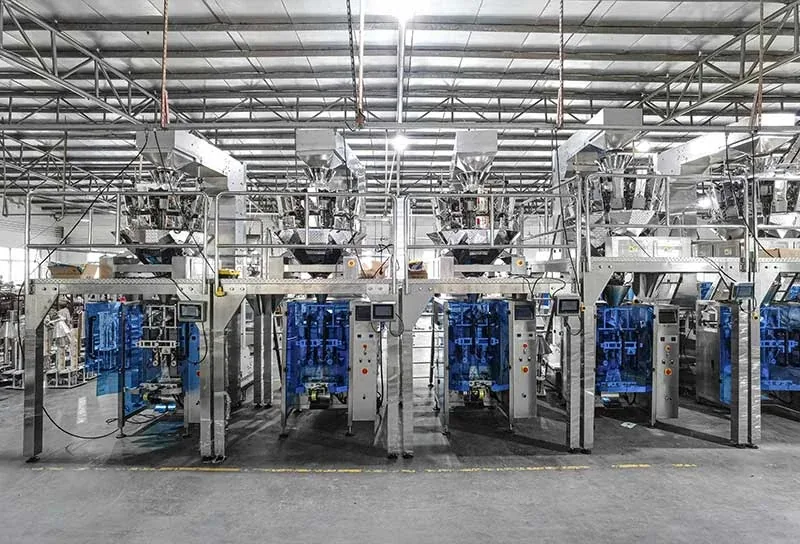
Every quotation issued by LINEVO includes our contractual 4-Gate Factory Acceptance Test (FAT) protocol executed on your physical packages and corrugated blanks prior to balance payment and shipment:
- Gate 1 — 30-Minute Continuous Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full nameplate speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Verified 15-Minute No-Tool Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels (
≤15 minutestotal elapsed time). - Gate 3 — Upstream & Downstream Interlock Simulation: We verify PackML dry-contact or Ethernet/IP handshakes with upstream checkweighers, metal detectors, downstream print-and-apply GS1-128 case labelers (
LV-9560PL), and24VMDR zero-pressure accumulation conveyors (≥60 secondsbuffer before palletizing).
To request a formal speed calculation, CAD layout, or FAT protocol for your line, message the LINEVO Engineering Review Board on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Discuss a technical specification on WhatsApp