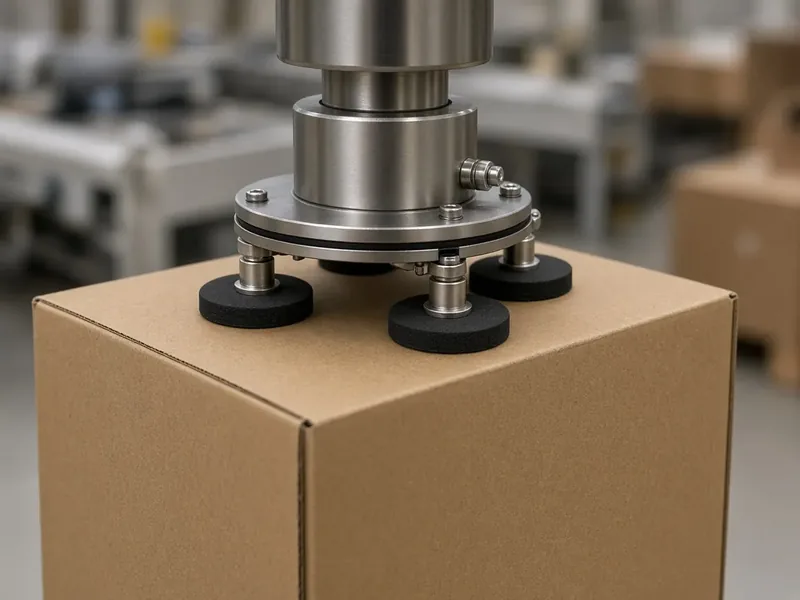
Every LINEVO secondary packaging machine must pass our documented 4-Gate Factory Acceptance Test (FAT) and corrugated jam prevention protocol on your production packages and knocked-down box blanks—verifying ≥98.5% completion over a 30-minute run at 100% rated CPM and a timed ≤15-minute no-tool SKU changeover.
Positive Pin-and-Dome vs Dual-Frame Vacuum Opening on Recycled Board
An automatic case packing line is only as reliable as its case erector and flap sealer: a 1.5% blank-opening misfire rate at 20 CPM stops the line every 3 minutes. Compare labor and consumable payback in our case packer cost and ROI calculator and enforce three corrugated handling standards:
- Overcoming High-Recycle Linerboard Porosity & Humidity Warp (
LV-CE200/LV-CE250): Standard single-side suction erectors (LV-CE150,8–12 CPM) lose vacuum grip when corrugated blanks exceed60%recycled fiber or±2.5 mmdiagonal warp. For12–18 CPMlines, theLV-CE200dual-frame opposition vacuum erector pulls both major panels simultaneously while over-breaking the score line to115°. For18–25+ CPMor100%recycled board, theLV-CE250positive pin-and-dome erector pierces the inner flute mechanically so porous or warped blanks (±4.5 mm) can never slip. - Hot-Melt Adhesive (
Nordson/Robatech) vs BOPP Tape (LV-FXC4030X): Pressure-sensitive48 mmor72 mmBOPP tape (LV-FXC4030X) requires zero warm-up time and suits8–18 CPMambient lines. Above1.0 million cases/year,NordsonorRobatechmetallocene hot-melt gluing (LV-HM400) cuts consumable cost by35% to 50%($0.012 vs $0.024 per case), forms a structural fiber-tear bond (≥80%) in1.5 seconds, and holds reliably in-25 °Cfreezer blast tunnels. - Corrugated Blank Specification Discipline (
FEFCO 0201,32–44 ECT): Specify±1.0 mmdie-cut score accuracy,40%–55%score-line depth, and flat-strapped inbound pallet bundles so knocked-down blanks feed smoothly from the powered horizontal walk-in magazine.
Compare related configurations and sizing tools across automatic case erectors and sealers, case erectors and case sealers, automatic case packers, corrugated box board quality for automatic case erectors, 15-minute no-tool changeover case packer design, automatic case packer manufacturer.
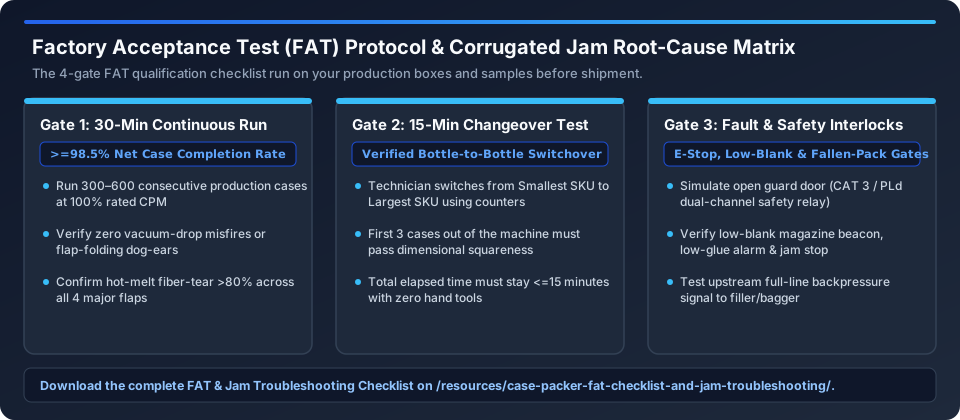
Case Erector & Sealer Performance Matrix & 4-Gate FAT Verification
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| Machine Station | LINEVO Model | Rated Speed (CPM) |
Opening / Sealing Mechanism | Board & SKU Envelope |
|---|---|---|---|---|
| Standard Vacuum Case Erector | LV-CE150 |
8–12 CPM |
Single-side Venturi vacuum + bottom tape head | Virgin / ≤50% recycled FEFCO 0201 RSC (32 ECT) |
| Dual-Frame Servo Case Erector | LV-CE200 |
12–18 CPM |
Opposing dual-side vacuum + 115° score over-break |
Up to 80% recycled board (±3.5 mm warp); tape or hot-melt |
| Pin-and-Dome High-Speed Erector | LV-CE250 |
18–25+ CPM |
Positive mechanical pin-and-dome retention + servo lugs | 100% recycled linerboard (±4.5 mm warp) at high speed |
| Uniform & Random Case Sealers | LV-FXC4030X / LV-HM400 |
10–30 CPM |
Rotary 4-flap kicker + side-belt drive (Tape or Hot-Melt) |
Uniform batch runs (1-min adjust) or Random auto-sensing |
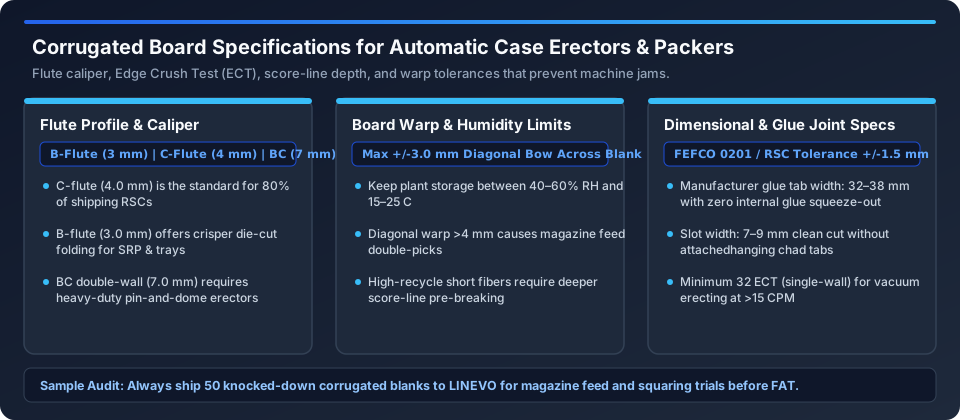
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Send my box drawing for a pre-FAT audit