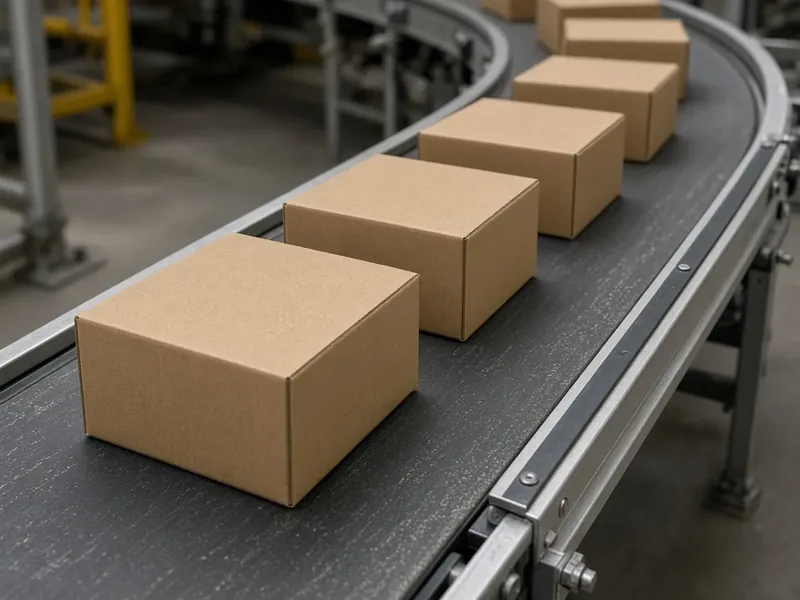
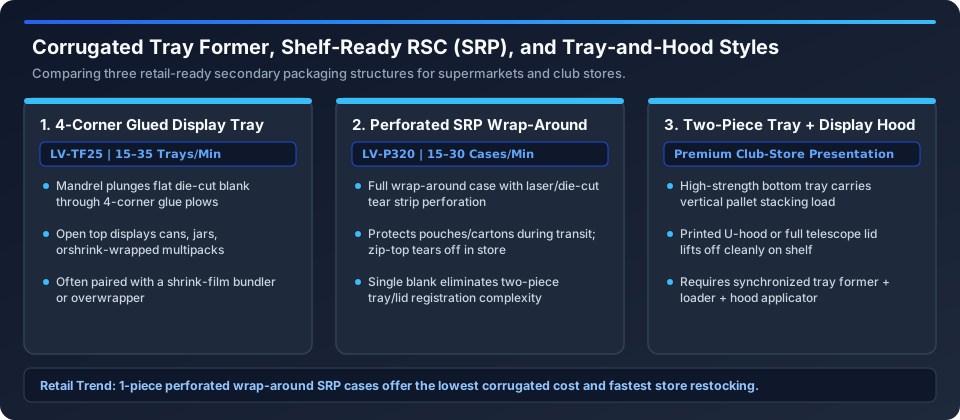
An automatic corrugated tray former and tray erector (LV-TF30, 15–35 trays/min) pulls flat die-cut corrugated blanks (FEFCO 0422 / 0452), applies Nordson or Robatech hot-melt adhesive to all four corner tabs, and squares rigid display and shrink-tunnel trays with a servo forming mandrel.
Wrap-Around Blank Folding Kinematics & 15%–22% Corrugated Board Savings
Unlike conventional erect-pack-seal systems that open a pre-glued FEFCO 0201 Regular Slotted Container (RSC) and require +4 to +6 mm of internal clearance so products can slide in, a LINEVO LV-P320 wrap-around and tray packer (15–30 CPM) feeds a flat die-cut corrugated blank (FEFCO 0409 or perforated SRP) and folds the board tightly around the collated product group. Audit your exact annual fiber savings in our wrap-around vs RSC corrugated cost calculator:
- 15% to 22% Corrugated Board Area Reduction: Eliminating the converter’s pre-glued manufacturer joint and replacing overlapping top/bottom RSC flaps with an outside glue tab cuts corrugated blank area by
15% to 22%per case—saving$0.06 to $0.14 per box($90,000 to $250,000+/yearon two-shift beverage, dairy, and canned food lines). - Zero Internal Clearance & Higher Stacking Compression (
BCT): Becauseservo folding plows and pneumatic mandrels wrap the corrugated walls directly against the product perimeter (0 mminternal gap), containers cannot rattle, scuff labels, or shift during transit, and vertical flutes stay perfectly plumb for pallet stacking. - 3-in-1 Format Flexibility (
Full Wrap-Around,Perforated SRP, andHalf-Tray): By recalling a servo HMI recipe and swapping quick-release pin mandrels in15 to 20 minutes, the sameLV-P320frame runs fully enclosed shipping cases, perforated tear-hood Shelf-Ready Packaging (SRP), and40–75 mmcorrugated display trays (LV-TF30).
Compare related configurations and sizing tools across automatic case packers, wrap-around and tray packers, case packer speed and collation calculator, case packer cost and ROI calculator, secondary packaging line footprint planner, case packer FAT checklist and jam troubleshooting manual.
Die-Cut Blank Tolerances, Hot-Melt Compression & 30 CPM Drive Architecture
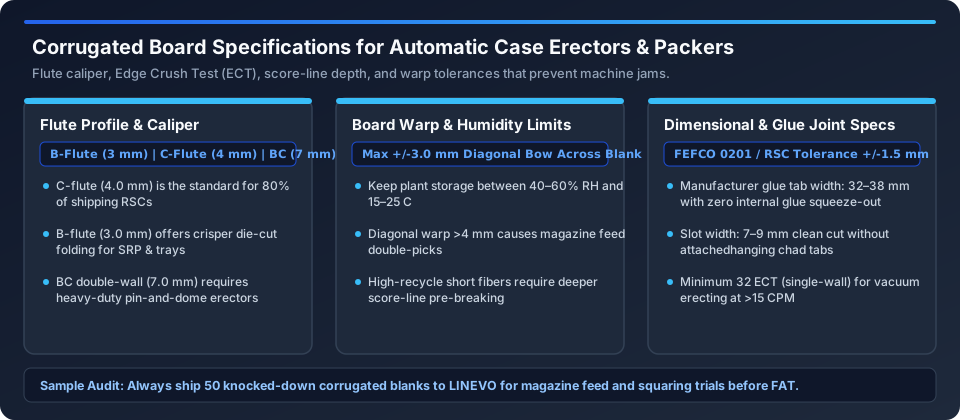
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| Engineering Parameter | Pre-Glued RSC Line (LV-CE250 + LV-P200) |
Continuous Wrap-Around & SRP Line (LV-P320, 15–30 CPM) |
Financial & Operational Impact |
|---|---|---|---|
| Corrugated Blank Format | Pre-glued knocked-down FEFCO 0201 RSC |
Flat die-cut FEFCO 0409 blank (B, C, or E flute, 32–44 ECT) |
35–40% more blanks per inbound pallet; zero converter gluing surcharge |
| Internal Pack Clearance | +4.0 to +6.0 mm required for insertion |
0.0 mm (tightly tension-wrapped around product group) |
Eliminates label abrasion and boosts pallet stack stability |
| Adhesive & Compression | Tape (LV-FXC4030X) or top/bottom hot-melt |
Nordson / Robatech metallocene hot-melt + servo Dual-Belt Compression |
1.5–2.0 s square hold guarantees ≥80% fiber tear at 30 CPM |
| SRP Tear-Strip Readiness | Difficult to load through pre-glued perforations | Flat blank folded without stressing zip-rule or twin-knife perforations | Clean 1-pull retail shelf hood removal with zero magazine jams |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Send my tray die-line drawing