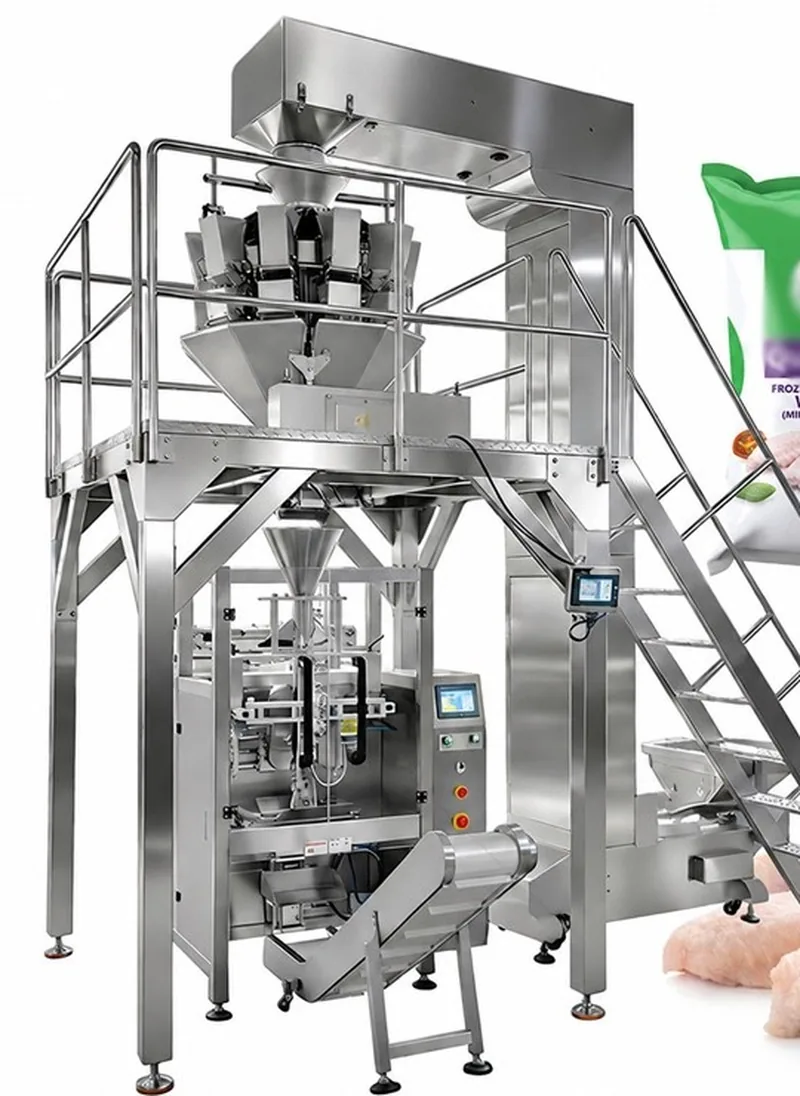
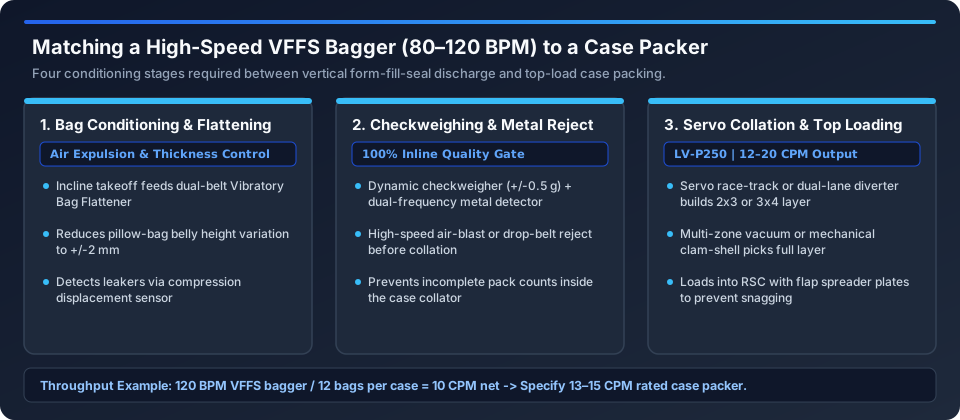
Matching an automatic case packer to a high-speed VFFS bagger (80 to 140 BPM) on snack, granola, frozen food, and powder lines requires a 4-stage conditioning train—incline take-away, vibratory bag flattener, checkweigher/metal-detector reject, and +20% to +25% OEE surge capacity—so downstream case packing never starves or stops the vertical bagger.
Infeed Bag Conditioning, Servo Collation & Pick-Head Cycle Math
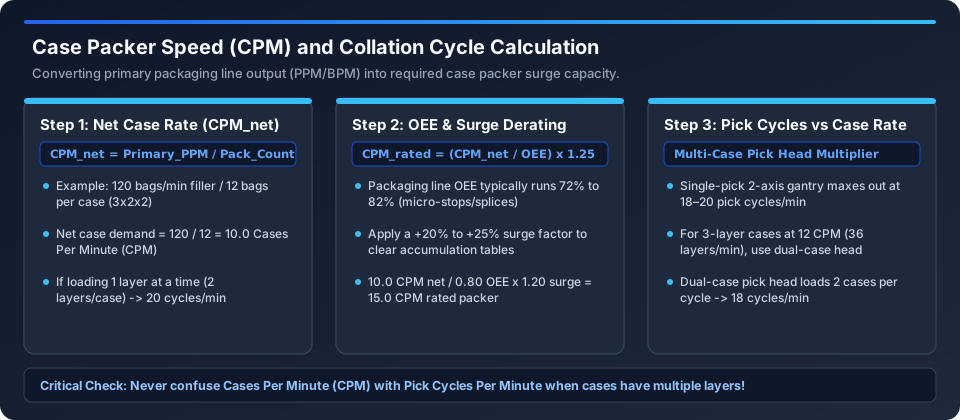
Flexible pouches and VFFS pillow bags (50 g to 3.0 kg) trap headspace air and shift center-of-gravity during high-speed transfer. Before selecting a frame, run your primary bagging rate (BPM) and pack matrix (Rows × Columns × Layers) through our case packer speed and collation calculator and enforce three mechanical rules:
- Vibratory Deaeration & Caliper Leveling (
±2.0 mm): Pouches discharging from an80–140 BPMvertical form-fill-seal bagger or horizontal premade pouch machine pass through an inclined take-away belt and a spring-mounted vibratory flattening conveyor (LV-BC120). Expelling trapped headspace air equalizes bag thickness within±2.0 mmso stacked layers never crown above the RSC flap score line. - Separating Case Throughput (
CPM) from Gantry Pick Cycles/Min: A 2-axis servo gantry (LV-P250) runs safely at15 to 20 pick cycles/min. On a single-layer case (L = 1),20 cycles/minyields20 CPM. On a 3-layer snack case (L = 3), a single pick head completes6.6 CPM—so lines requiring14 to 20 CPMon multi-layer pouch cases specify theLV-P250-2Cdual-case pick head (loading two cases simultaneously) or aLV-RD1204-axis Delta vision cell (60–120 picks/min). - Multi-Zone Vacuum Bellows vs Clamshell Cradle Tooling: Smooth laminate pillow bags below
1.0 kgusePiab/Schmalzmulti-stage Venturi silicone bellows with independent check valves. Heavy liquid pouches (1.5–5.0 kg), dusty powder bags, or stand-up Doypacks packed vertically (SRP) use servo clamshell fingers and diving partitioning plates so zero vacuum tension is applied to the top heat seal.
Compare related configurations and sizing tools across automatic case packers, top-load and pick-and-place case packers, wrap-around vs RSC corrugated cost calculator, case packer cost and ROI calculator, secondary packaging line footprint planner, case packer FAT checklist and jam troubleshooting manual.
RSC Blank Squaring, Diving Funnel Guides & 15-Minute Changeover
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| Subsystem Parameter | Standard Pouch Line (LV-P250, 8–14 CPM) |
High-Speed / Multi-Layer Line (LV-P250-2C / LV-RD120, 15–22 CPM) |
Operational Verification Standard |
|---|---|---|---|
| Top-Load Diving Funnel | 4-sided pneumatic stainless entry shroud | Servo-synchronized diving funnel that enters 25 mm inside RSC walls |
Isolates all 4 top flaps so flexible bag corners never snag during drop |
| Blank Erecting & Squaring | Dual-frame opposition Venturi vacuum (LV-CE200) |
Positive mechanical pin-and-dome (LV-CE250) for recycled board |
Holds 90.0° ± 1.0° corner squareness on 100% recycled board (±4.0 mm warp) |
| Flap Closing & Sealing | 48/72 mm BOPP pressure-sensitive tape (LV-FXC4030X) |
Nordson or Robatech metallocene hot-melt glue (1.5–2.5 g/case) |
Achieves ≥80% fiber-tear bond in 1.5 s and cuts consumable cost by 40% |
| SMED No-Tool Changeover | Siko 4-digit digital counters + quick-release funnel pins (≤15 min) |
Servo auto-adjusting collator rails + 100-recipe HMI recall (≤10 min) |
First case out after SKU switch meets ±1.5 mm diagonal squareness |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Match a case packer to my VFFS speed