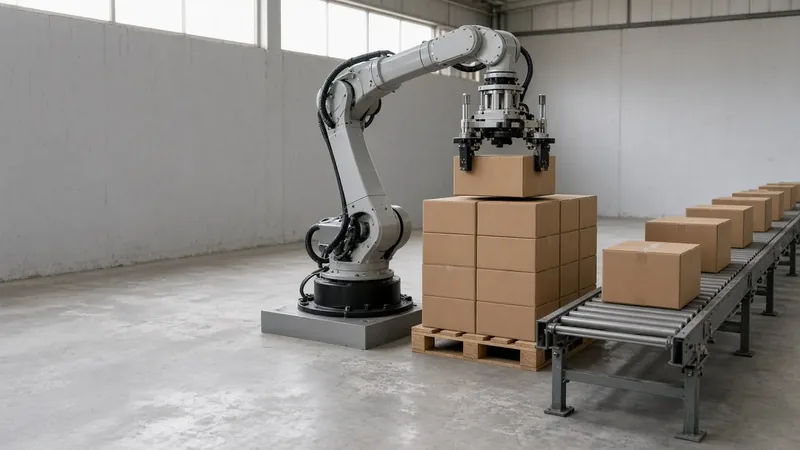
Engineering robotic case palletizing directly downstream of your case packer (LV-RP200, 8–28 CPM) matches multi-case EOAT (zoned foam vacuum, pneumatic side-clamp, or under-support comb fork) and dual-bay pallet dispensing to your upstream case sealer discharge.
Synchronizing Case Sealing, GS1-128 Labeling, Accumulation & Palletizing
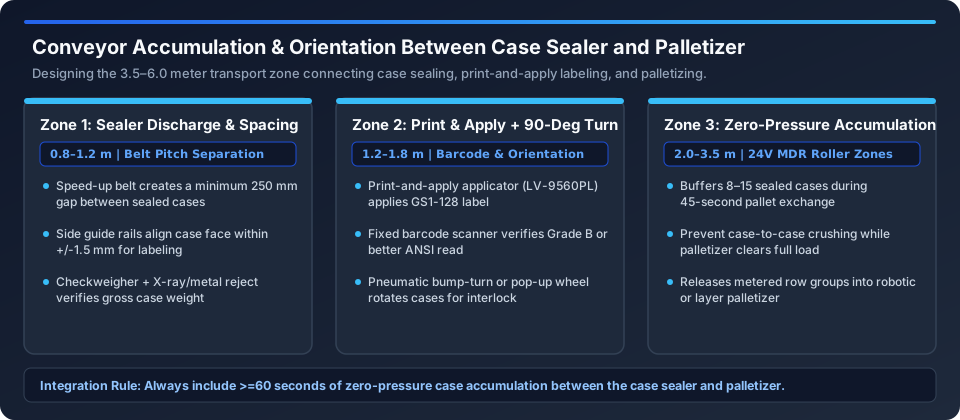
An automatic case packer cannot achieve its rated shift OEE if downstream bottlenecks—such as a label roll change, a pallet exchange pause (45 seconds), or a stretch-wrapper cycle—back up cases into the sealer discharge. Plan your complete end-of-line layout in our secondary packaging line footprint planner and enforce three integration standards:
- 60-Second Zero-Pressure MDR Accumulation Buffer: Between the case sealer discharge (
LV-FXC4030X/LV-HM400) and the palletizer infeed, LINEVO installs3.5 to 6.0 metersof24Vmotorized drive roller (MDR) zero-pressure accumulation conveyor. When the palletizer pauses for30–45 secondsto discharge a full pallet and dispense an empty wood pallet (LV-PD10), the case packer continues running at100%speed without stopping the upstream filler. - Inline Print-and-Apply GS1-128 Case Labeling (
LV-9560PL): Immediately after flap sealing and checkweighing, a servo tamp-blow or corner-wrap print-and-apply labeler (LV-9560PLwithZebraZE511orSatoS84-ex300 DPIthermal-transfer engine) applies serialized GS1-128 labels (32 mmfrom base,≥19 mmfrom vertical edge) and verifiesISO/IEC 15416 Grade B (≥2.5)barcode readability via fixed-mount scanner. - Matching Robotic (
LV-RP200) vs High-Level Layer (LV-HL300) Palletizers: For6–25 CPMlines or multi-line central cells, a 4-axis robotic palletizer (LV-RP200) with vacuum, side-clamp, or bottom-fork EOAT stacks cases to±1.5 mmaccuracy. Above25–50+ CPM, a high-level row-forming stripper-apron palletizer (LV-HL300) forms and squares full layers continuously.
Compare related configurations and sizing tools across automatic case packers, palletizers for case packing lines, case packer speed and collation calculator, wrap-around vs RSC corrugated cost calculator, case packer cost and ROI calculator, case packer FAT checklist and jam troubleshooting manual.
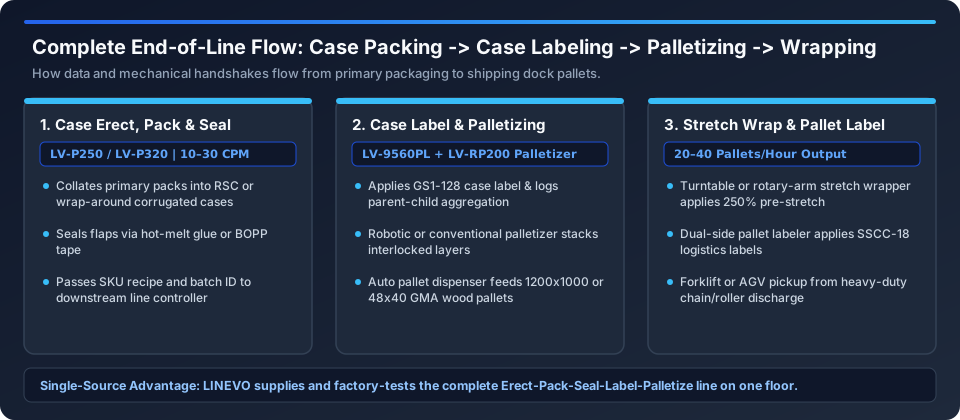
Turnkey End-of-Line Handshake Architecture & Single-OEM FAT Protocol
Even the fastest servo collator will miss shift OEE targets if the case erecting, flap sealing, or downstream accumulation module jams on high-recycle corrugated board. LINEVO enforces four mechanical design standards across every station:
| End-of-Line Module | LINEVO Model | Speed Envelope | Mechanical & Data Handshake | Turnkey Integration Benefit |
|---|---|---|---|---|
| Print-and-Apply Case Labeler | LV-9560PL |
15–40 CPM |
Encoder-tracked wipe/tamp/corner-wrap + inline barcode verifier | Zero unverified GS1-128 cases reach the palletizer |
| MDR Accumulation & Turning | LV-MDR60 |
60–90 s buffer |
Photo-eye zoned 24V zero-pressure rollers + bump-turn orientation |
Absorbs pallet exchanges without stopping case packer |
| Robotic / Layer Palletizer | LV-RP200 / LV-HL300 |
8–50+ CPM |
Automatic pallet dispenser (LV-PD10) + slip-sheet inserter |
Stacks column or interlock Ti-Hi patterns within ±1.5 mm |
| Rotary Ring Stretch Wrapper | LV-SW40 + LV-PL100 |
20–45 pallets/hr |
250% powered pre-stretch + 2-panel SSCC-18 pallet labeler |
Delivers dock-ready, retailer-compliant unit loads |
4-Gate Factory Acceptance Testing (FAT) & Turnkey Line Qualification
Before any LINEVO case packer, case erector, or integrated monoblock (LV-P200-MP) is approved for crating, our engineering team executes a documented 4-Gate Factory Acceptance Test (FAT) using 30 to 50 of your actual knocked-down corrugated blanks and production product samples:
- Gate 1 — 30-Minute Uninterrupted Run at 100% Rated CPM: The machine packs
300 to 900 consecutive casesat full contract speed with≥98.5%net completion, zero vacuum-drop misfires, and≥80%hot-melt fiber tear across all four major flaps. - Gate 2 — Timed ≤15-Minute No-Tool SKU Changeover: A single technician switches the machine from your smallest SKU to your largest SKU using only the Siko digital counter recipe sheet and quick-release pin mandrels, verifying first-case diagonal squareness within
±1.5 mm. - Gate 3 — PackML Upstream & Downstream Handshake Simulation: Full verification of dry-contact or Ethernet/IP / Profinet interlocks with upstream checkweighers, metal detectors, downstream
LV-9560PLprint-and-apply GS1-128 labelers, and24VMDR accumulation conveyors.
To get a formal cycle-rate calculation, CAD floor layout, and itemized engineering quotation for your package and box drawing, message our LINEVO engineering team directly on WhatsApp.
Get a Case Packing Route Checked Against Your Box Samples
Send your primary package dimensions, pack pattern (R × C × L) and target CPM on WhatsApp. LINEVO engineers will propose a case packing layout and the FAT checks to run on your corrugated blanks.
Match a robotic palletizer to my case packer